


Inspection and Detection Solutions
Applications: food and beverage industry, pharmaceutical industry, automotive industry, cosmetics etc.
Metals detection and inspection solutions
- CEIA solutions detect metal contaminants with levels of sensitivity, interference immunity, and response speeds that exceed the strictest quality control standards
- Have compact dimensions with extremely high energy efficiency and long-term reliability
- Use the most advanced electronic and mechanical technologies
- CEIA metal detectors are certified ISO 9001 and manufactured from materials approved by the EC and FDA
- Uses multispectral technology that selects and uses at the same time a set of detection frequencies tailored to the product and packaging


Metals inspection and detection
- CEIA solutions detect metal contaminants with levels of sensitivity, interference immunity, and response speeds that exceed the strictest quality control standards
- Have compact dimensions with extremely high energy efficiency and long-term reliability
- Use the most advanced electronic and mechanical technologies
- CEIA metal detectors are certified ISO 9001 and manufactured from materials approved by the EC and FDA
- Uses multispectral technology that selects and uses at the same time a set of detection frequencies tailored to the product and packaging


X-ray inspection and detection from Wipotec OCS
- X-rays can penetrate materials that do not allow any visible light to pass through. This means greater safety and quality for your production as X-ray inspection systems enable you to track down hidden contaminants such as glass, bones, stones, or metal quickly and easily. As foreign bodies absorb more X-rays than the food surrounding them, they are easy to find and eject.
- A reliable equipment for foreign body detection and visual inspection
- Hygienic design to meet the highest hygiene and safety requirements
- Modular equipment for rapid solution development
- Smart software that covers a wide range of applications
Applications: foreign body detection (ferrous/non-ferrous metals, stones, bones, glass, Teflon), completeness check, filling level check, shape and position check, position and distribution check, clip recognition (missing clip), defects inspection.
Applications in the food industry (ready meals, coffee & tea, pet food, cheese, sweets, dairy, spices & instant meals, meat & sausages, fish & seafood, bread, and bakery), pharmaceutical industry, cosmetics industry.

Inspection and detection with vision systems
The benefits of vision systems in the product inspection:
- Detect damaged products
- Reduce costly downtime and manual intervention
- Avoid packaging mix-ups
- Preserve customer loyalty
Vision applications in product quality inspection:
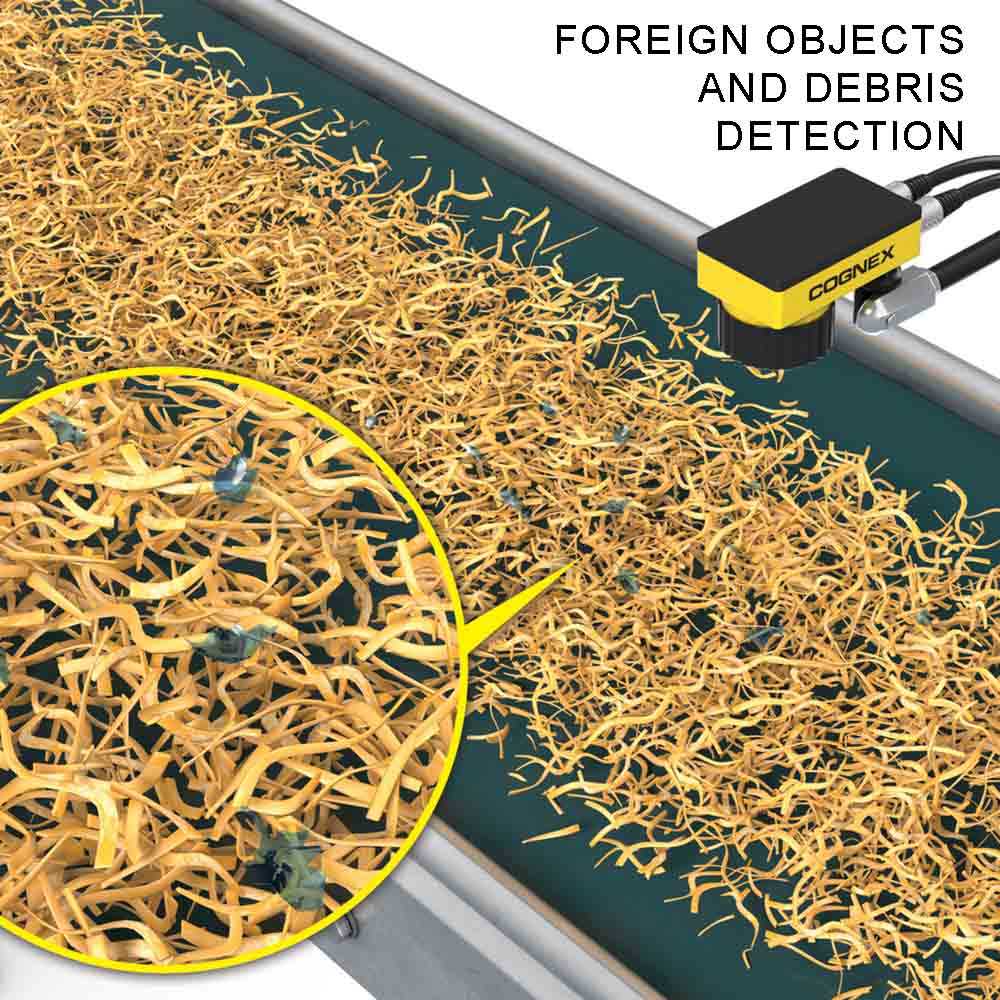
- Detect foreign objects and debris
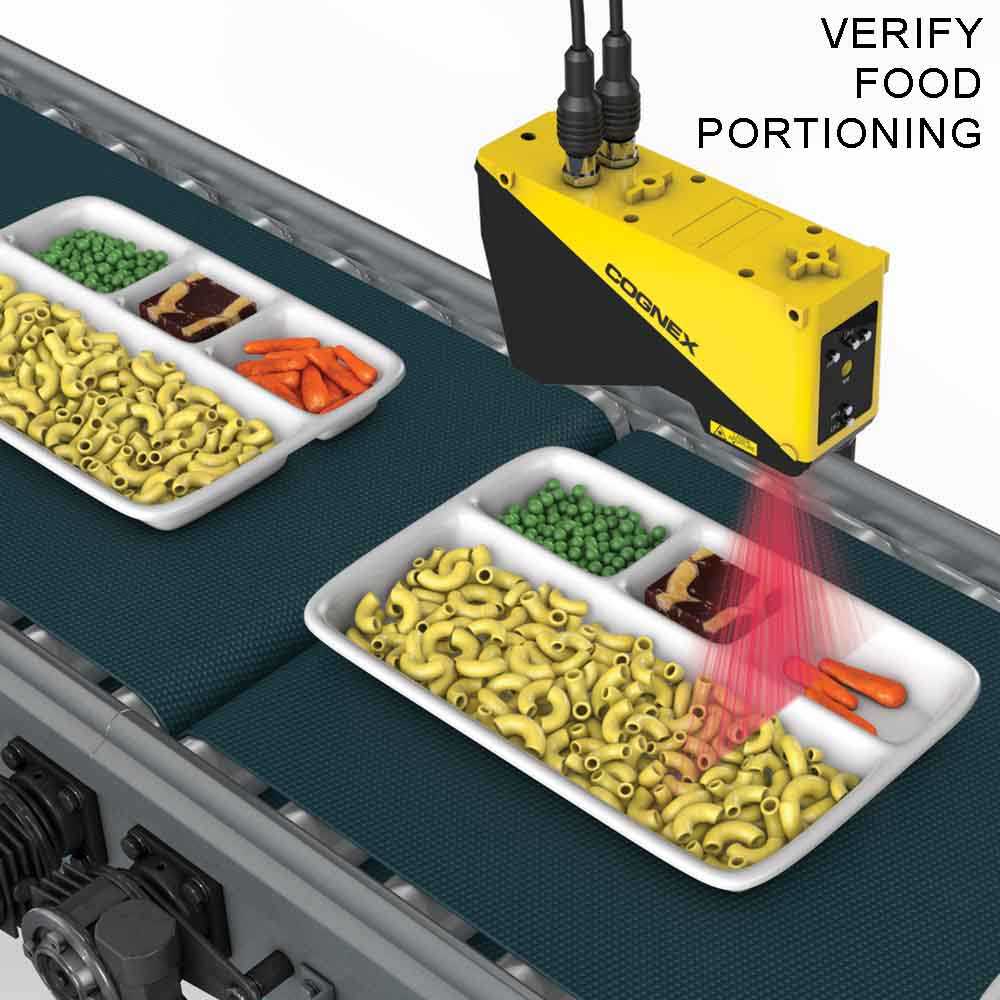
- Verify food portioning
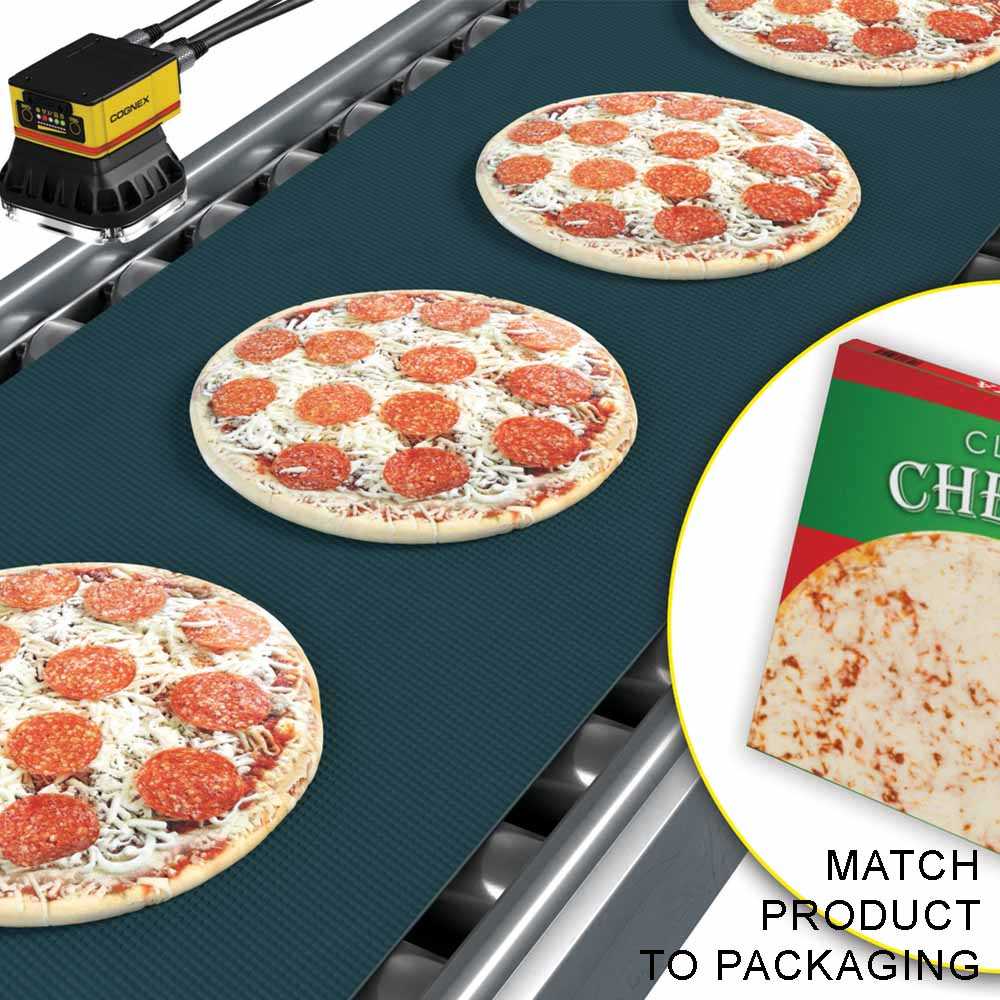
- Match product to packaging
- Ensure consistent size, shape, color, and texture
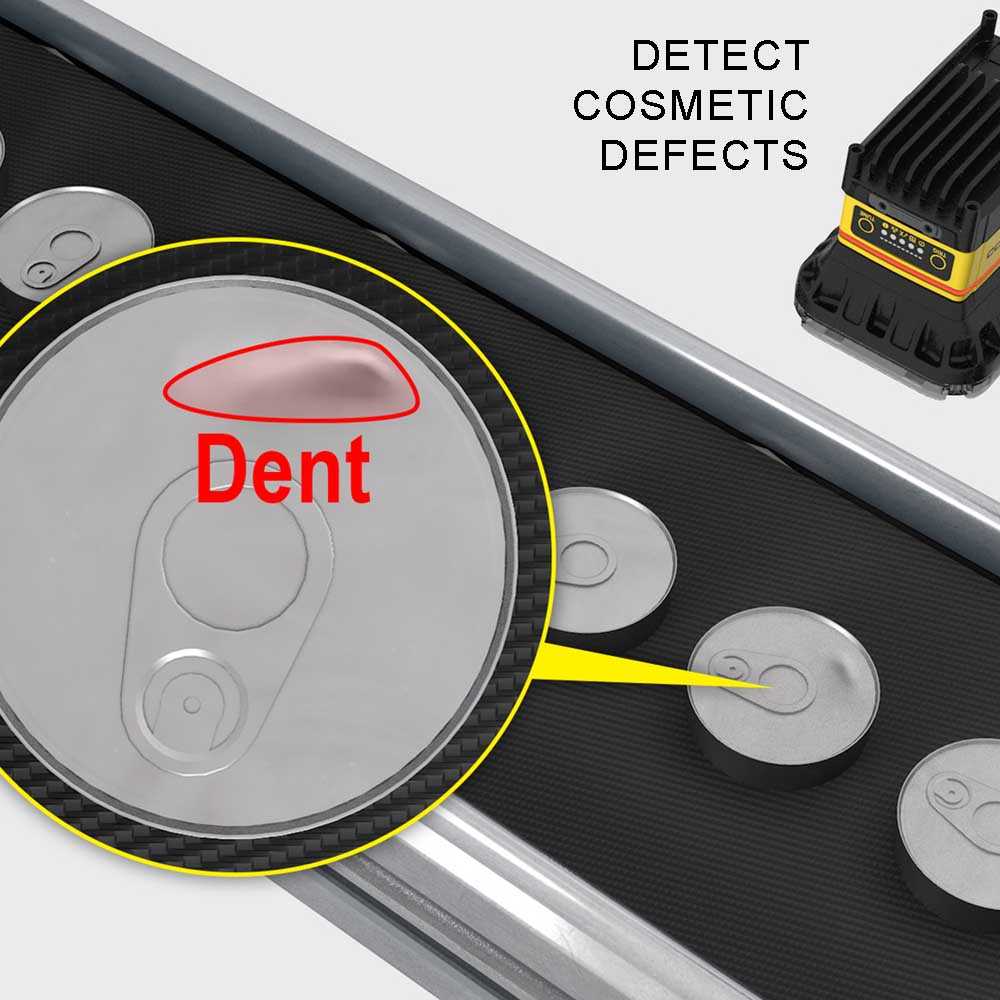
- Detect cosmetic defects
- Automate classification


Inspection and detection with vision systems
The benefits of vision systems in the product inspection:
- Detect damaged products
- Reduce costly downtime and manual intervention
- Avoid packaging mix-ups
- Preserve customer loyalty
Vision applications in product quality inspection:
- Detect foreign objects and debris
- Verify food portioning
- Match product to packaging
- Ensure consistent size, shape, color, and texture
- Detect cosmetic defects
- Automate classification


Packaging Testing Solutions – Advanced Control of Seal Integrity and Modified Atmosphere
Oxylos – Automatic instrument for package leak testing and gas analysis (O₂ and CO₂)
Exos – MANUAL instrument for package leak testing and gas analysis (O₂ and CO₂)
Ipos 2 – Instrument for gas analysis (O₂ and CO₂)
Why choose these instruments for package leak testing and MAP verification?
- Made in France
- Can be integrated into your production lines
- Multiple test types with a single analyzer:
- Leak testing
- Gas concentration verification
- Burst strength testing
- Each test can be performed consecutively or independently, depending on your product specifications
- User-friendly, robust, and cost-effective
Designed to meet the strict requirements of safety and traceability in critical industries such as:
- Food industry: meat, fish, dairy, bakery, snacks, vegetables
- Pharmaceutical industry: blister packs, sachets, vials
- Industrial packaging: pouches with components sensitive to moisture or gases
- Quality control and R&D laboratories
Benefits:
- Enhanced product safety and extended shelf life
- Early detection of packaging defects
- Compliance with international packaging and food safety regulations
- Optimized production processes and reduced waste


